Hobart Commercial Food Preparation and Warewashing Systems
Engineered with heavy-duty induction motors and rugged stainless steel gear-driven transmissions, premium hobart mixers deliver absolute mechanical processing torque for continuous commercial kitchen operations. We distribute these high-performance culinary systems and industrial Hobart mixers featuring planetary gear configurations, integrated safety guard interlocks, and digital timer modules. Choosing Hobart eliminates transmission gear stripping and motor stalling, outperforming standard light-duty prep appliances through massive cast aluminum housings and severe-service engineering parameters.
This professional-grade food preparation machinery is custom-built for high-volume bakeries, institutional cafeteria kitchens, commercial restaurants, and meat processing facilities. Our catalog features robust commercial kitchen hardware designed to plug directly into your automated food service Hobart food processors layout to maximize meal preparation yields and accelerate daily kitchen prep cycles. Upgrade your commercial culinary infrastructure today with competitive commercial contract pricing, rapid freight shipping, and extended factory warranties on all powertrain gearboxes.
Hobart Professional Commercial Kitchen Features
- Planetary Food Mixers: High-capacity commercial mixers utilizing fixed steel bowls and rotating tool pins to ensure deep, consistent batch kneading.
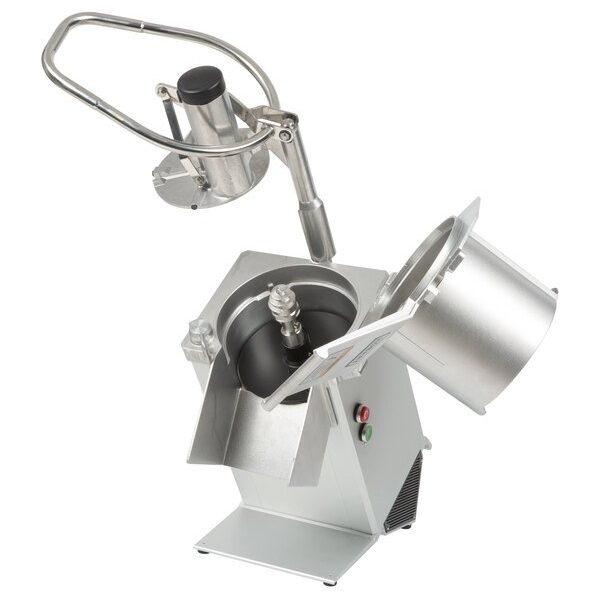
- Continuous Food Processors: Industrial direct-drive vegetable cutters utilizing large-diameter plates to slice tons of ingredients rapidly.
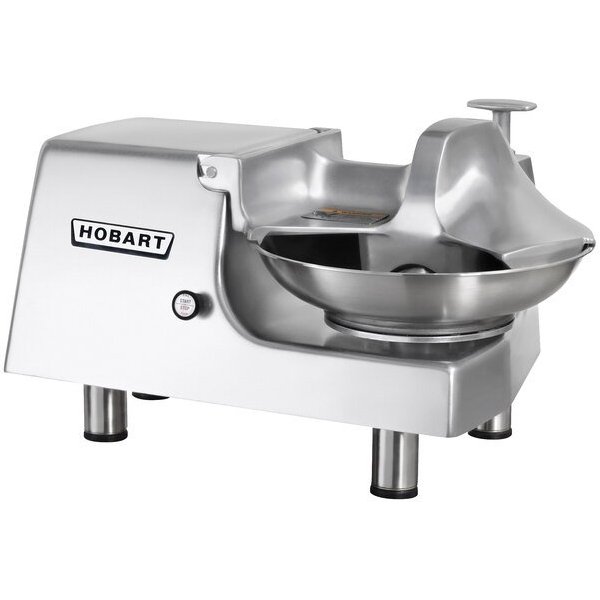
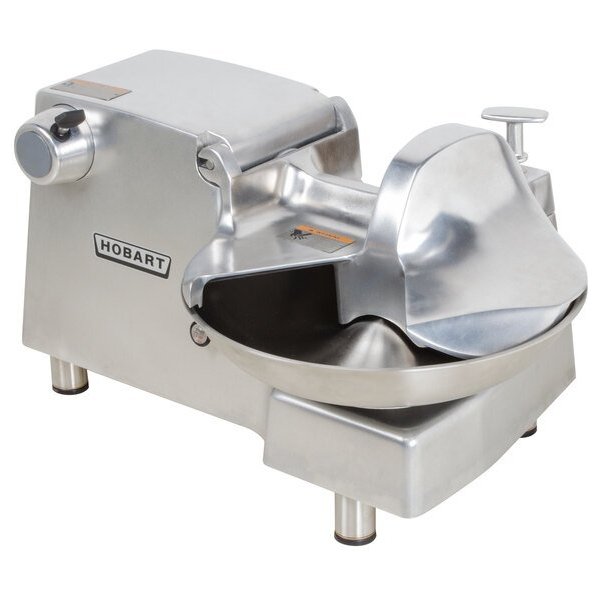
- Commercial Bowl Cutters: Heavy-gauge stainless steel rotating bowls matched with high-speed blades designed to chop and emulsify meats smoothly.
- Industrial Warewashers: High-temperature sanitize dishwashers utilizing integrated booster heaters to eliminate food soils completely.
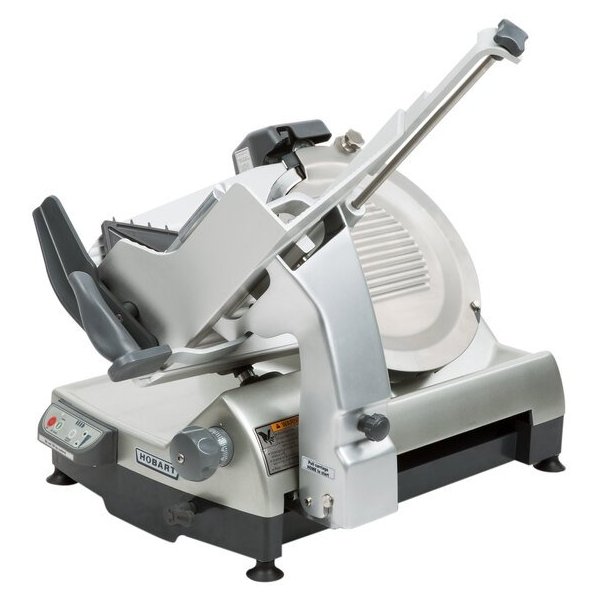
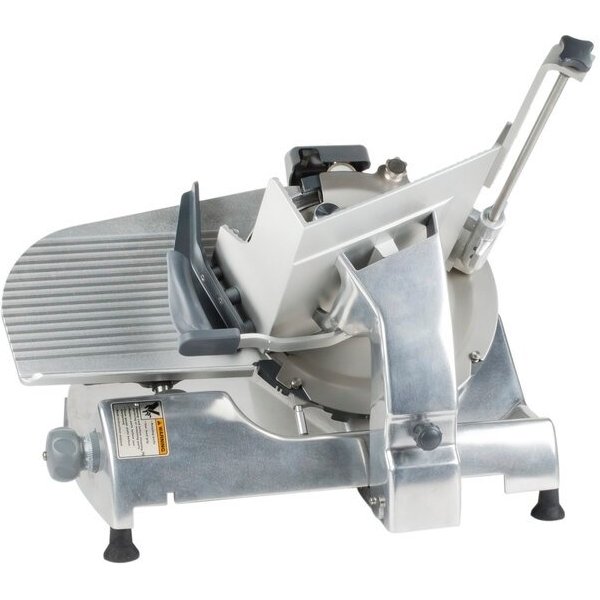
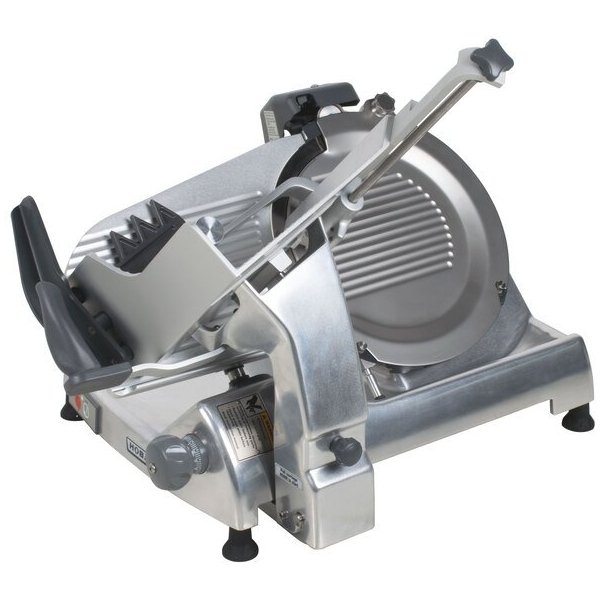
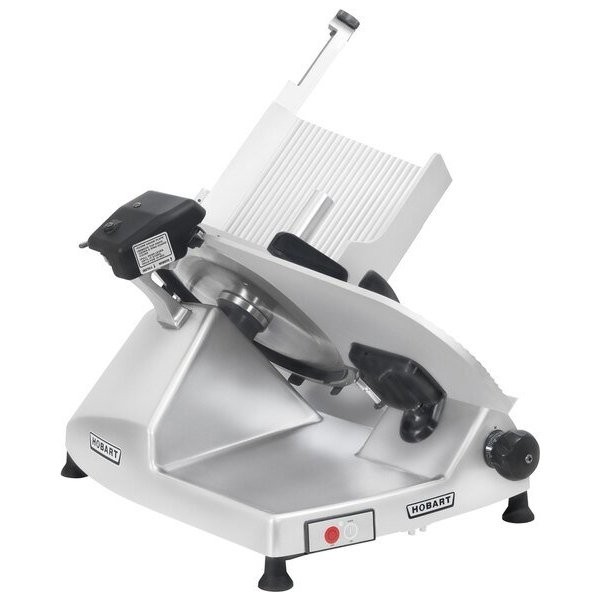
- Heavy-Capacity Meat Slicers: Hard-chromed carbon steel blades equipped with integrated knife-sharpening stones for clean cutting accuracy.
Technical Questions Regarding Hobart Equipment
Why are gear-driven transmissions superior to belt drives in Hobart industrial planetary mixers?
Hobart builds its mixers using an all-metal gear-driven transmission system that locks heavy steel gears directly to the drive shaft, completely removing rubber belts that stretch and slip under stress. This layout captures 100% of motor torque, allowing the mixing head to knead dense bread dough without heat spikes or mechanical speed drops.
How does the integrated bowl interlock safety mechanism protect Hobart mixer operators?
The proprietary Hobart safety system places solid-state electronic proximity sensors inside both the bowl support carriage and the wire cage splash guard. If an operator drops the bowl or shifts the cage during a batch cycle, the electrical circuit instantly cuts power, bringing the motor shaft to a complete mechanical stop within a second.
Do Hobart commercial kitchen appliances satisfy national foodservice sanitation codes?
Yes, all authentic Hobart commercial processing and washing units are fully engineered to meet strict NSF International sanitation standards and carry ETL marks. The seamless stainless steel components and chemical-resistant alloys eliminate bacteria harbor points, ensuring trouble-free municipal health inspections.
Showing 1–20 of 46 resultsSorted by latest